
Root Cause Failure Analysis Lab
Root cause failure analysis for metals, polymers, ceramics, semiconductors and electronic assemblies, from an ISO/IEC 17025-accredited lab in Silicon Valley.
When a part cracks, corrodes, delaminates or stops working, you need to know why. Often you also need evidence that a customer, supplier or court will accept. Our failure analysis lab pairs 75+ analytical instruments with materials scientists who run each investigation from the first inspection to the final report.
What Is Failure Analysis?
Failure analysis is the systematic investigation of why a component, material or product failed. It uses visual inspection, nondestructive testing, microscopy and chemical analysis to identify the failure mode, the mechanism behind it and the root cause, so engineers can correct the problem and keep it from happening again.
An investigation works through three questions in order. First, what happened: the failure mode, such as a fatigue fracture or a short circuit. Second, how it happened: the mechanism, such as cyclic loading concentrated at an undersized fillet radius. Third, why it happened: the design, material, process or service condition that allowed it. Investigations that stop at the failure mode often produce fixes that don't hold.

When to Order a Failure Analysis
- A part fails in the field, in qualification testing or on the line, and the cause isn't obvious
- Warranty returns or customer complaints cluster around one product, lot or supplier
- Yield drops and your process controls don't explain it
- You see cracking, corrosion, discoloration, delamination, residue or contamination
- A supplier dispute, insurance claim or lawsuit needs independent, documented evidence
- You're qualifying a new material, supplier or process and want to see how it fails before it reaches customers
Types of Failure We Investigate
Failure type | Typical signs | Techniques we use |
|---|---|---|
Fracture and fatigue | Cracks, beach marks, sudden breakage, ductile or brittle fracture surfaces | Stereo microscopy, SEM fractography, metallographic cross-sections, hardness, tensile testing |
Corrosion and environmental cracking | Pitting, stress corrosion cracking (SCC), hydrogen embrittlement, galvanic attack | SEM-EDS, XPS, XRD, cross-sections, Auger |
Contamination and residues | Haze, films, particles, adhesion loss, outgassing | FTIR, Raman, ToF-SIMS, XPS, GC-MS, SEM-EDS |
Coating and adhesion failures | Delamination, blistering, peeling, poor bonding | Cross-sections, SAM, XPS depth profiling, contact angle, FIB-SEM |
Polymer and plastic failures | Embrittlement, crazing, warping, discoloration, chemical attack | FTIR, DSC, TGA, DMA, GPC, SEM |
Electronic and semiconductor failures | Opens, shorts, leakage, EOS/ESD damage, solder joint cracks, voids | 2D X-ray, micro-CT, SAM, FIB-SEM, TEM, cross-sections |
Manufacturing and process defects | Porosity, inclusions, voids, weld defects, out-of-spec dimensions | Micro-CT, metallography, optical profilometry, white light interferometry |
Thermal damage | Overheating, warpage, CTE mismatch, thermal cycling cracks | TMA, DSC, TGA, cross-sections, SEM |
Our Failure Analysis Process
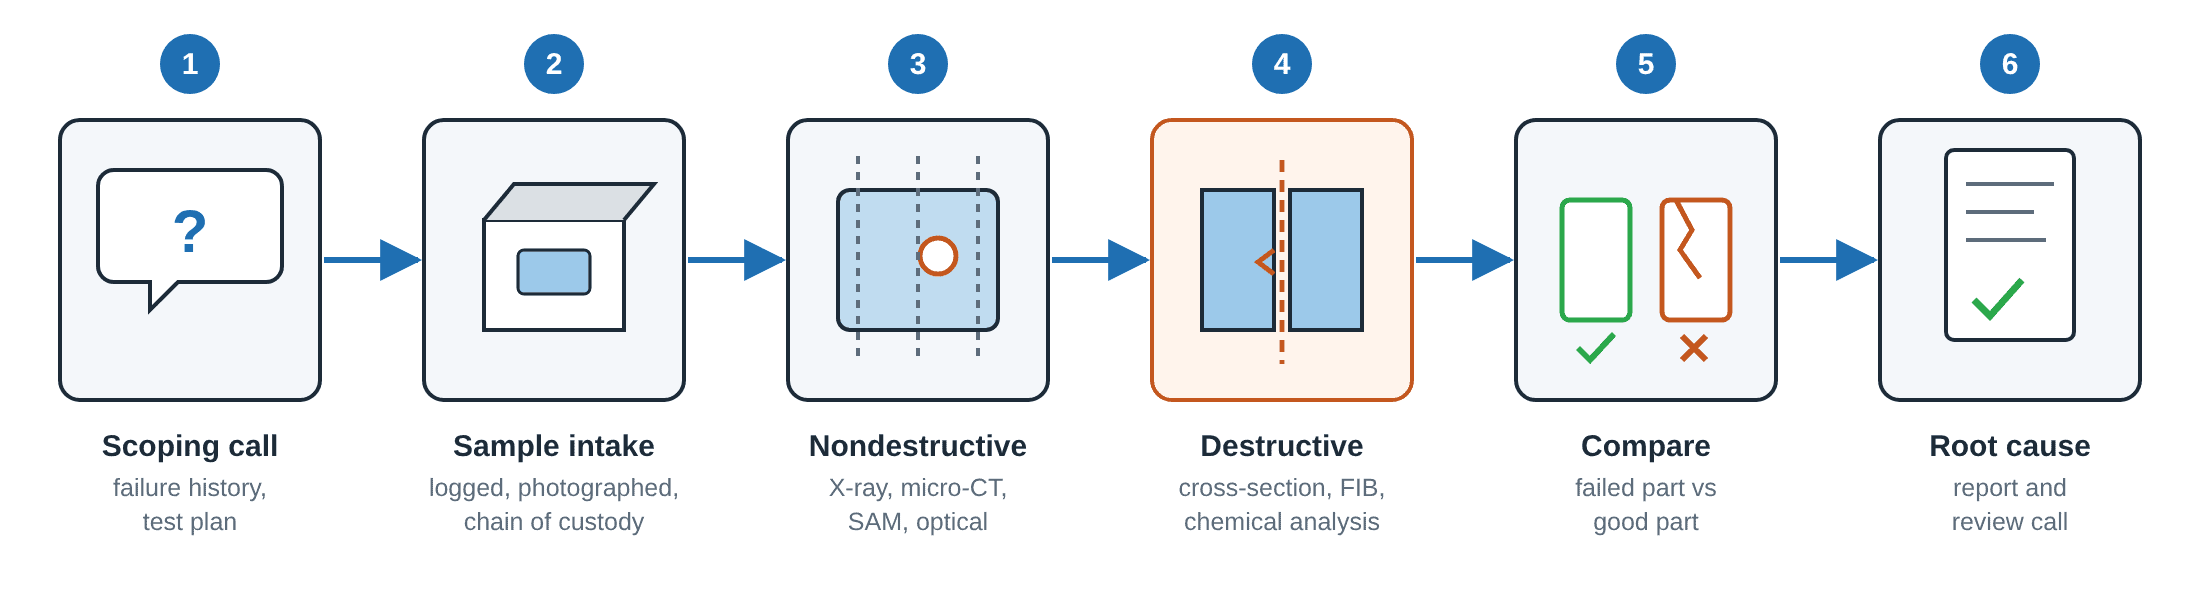
Each investigation moves from nondestructive to destructive methods, so the evidence is documented before anything is cut or altered.
It starts with a scoping call (1). A materials scientist reviews the failure history, the service conditions and the decision you need to make, then sends a test plan and quote. When samples arrive (2), we log and photograph them, and chain-of-custody documentation is available for legal and insurance work.
Nondestructive examination comes next (3). Optical inspection, 2D X-ray, micro-CT and scanning acoustic microscopy locate the defect without changing it. Then targeted destructive analysis (4) uses cross-sectioning, FIB-SEM, fractography and chemical analysis at the failure site. If you can send a passing part, we test it alongside the failed one (5) to separate the cause from normal part-to-part variation.
You get a written report (6) with annotated images, the data, the failure mechanism, the most likely root cause and recommended corrective actions. The scientist who ran the work then walks you through it on a call.
Failure Analysis Techniques
Most failure analysis work runs on the 75+ instruments in our Sunnyvale lab, so an investigation can move from X-ray to FIB to surface chemistry without waiting on another facility. When a case needs a technique we don't run in-house, we send that part of the work to a partner lab in our Covalent Connect network. You still work with one Covalent scientist and get one report.
- Microscopy: SEM, TEM, FIB-SEM, optical and stereo microscopy, white light interferometry
- Nondestructive inspection: 2D X-ray inspection, micro-CT, scanning acoustic microscopy (SAM)
- Elemental and surface chemistry: SEM-EDS, XPS, ToF-SIMS, Auger, XRF
- Molecular and organic analysis: FTIR, Raman, GC-MS
- Structure and phase: XRD, metallography, mechanical cross-section analysis
- Thermal and mechanical: DSC, TGA, DMA, TMA, hardness, tensile testing
Industries we support
| Industry | Typical failure analysis work |
|---|---|
| Semiconductor | Device failure analysis at die and package level, delamination, wire bond and bump failures, contamination from process tools |
| Electronics and PCBA | Solder joint fatigue, conductive anodic filament, voiding, connector corrosion |
| Medical devices | Implant and component fractures, polymer degradation, residues relevant to biocompatibility |
| Aerospace and defense | Fatigue and corrosion in structural metals, coating failures, composite delamination |
| Energy and batteries | Electrode and separator failures, lithium plating, cell swelling, solar module degradation |
| Industrial and consumer products | Cracked housings, failed fasteners and welds, wear, contamination |
Failure Analysis Services at Covalent
Our 30,000 ft² lab holds 75+ instruments and more than $25M in instrumentation, so the test plan can follow what the evidence shows. The lab is accredited to ISO/IEC 17025 across 60+ analytical methods, 70% of our staff hold PhDs or advanced degrees, and more than 1,500 companies have sent us work.
You talk directly to the scientist running your samples. Every report includes a plain-language root cause summary, annotated images with the raw data, corrective action recommendations and a review call with that scientist. Chain-of-custody documentation for warranty, insurance, IP or litigation support is available on request. For techniques we don’t run in-house, we can place work through Covalent Connect, our network of trusted partner labs.
Turnaround is typically 5–7 business days, with rush options available at an extra cost.
Frequently Asked Questions
How long does failure analysis take?
Turnaround is typically 5–7 business days, with rush options available at an extra cost. Complex investigations with several techniques may take longer, and we confirm the timeline when we scope the project.
Do you disassemble failed parts and prepare the samples?
Yes. Our team handles disassembly and every stage of sample preparation, including cross-sectioning, polishing and FIB preparation.
What are the warning signs that I need failure analysis right away?
Sudden breakdowns, abnormal electrical or mechanical behavior, or unexplained contamination or defects. Other signs include recurring failures despite process controls, visible cracks or delamination, and significant yield losses.
Can you help with litigation or insurance claims?
Yes. Failure analysis results can support forensic investigations for insurance claims, warranty disputes, intellectual property protection and legal proceedings. You receive a detailed, documented report with high-resolution images and expert interpretation, and chain-of-custody documentation is available.
What information should I include when submitting a failed sample?
Include as much context as possible:
- Service conditions, such as temperature, load and chemical exposure
- How long the part was in use
- The failure symptoms you observed
- Drawings or specifications, if available
- Safety documentation, if relevant
What is the difference between a failure mode and a root cause?
The failure mode is what happened, such as a fatigue crack. The root cause is why it happened, such as an undersized fillet radius or a material defect. Fixing only the failure mode often leads to repeat failures.